Top 10 Essential Chemical Equipment for Global Buyers?
In the world of Chemical Equipment, selecting the right tools is crucial for efficiency and safety. Dr. Emily Carter, a leading expert in chemical engineering, once stated, "The right equipment can make or break your project." This highlights the significance of understanding essential equipment for global buyers.
The industry is diverse, with numerous options available. From reactors to separators, the choices can seem overwhelming. Understanding each piece's role will empower users to make informed decisions. Equipment quality impacts productivity and safety, affecting operations at all levels.
Despite advancements, challenges remain. Some equipment may not meet specific project needs. Buyers must navigate these challenges while ensuring compliance with safety standards. In this dynamic field, continuous learning and adaptation become critical for success.
Top 10 Essential Chemical Equipment for Global Buyers
In the competitive landscape of chemical manufacturing, selecting the right equipment is crucial. Recent industry reports indicate that the global chemical processing equipment market is projected to reach over $650 billion by 2026, growing at a CAGR of around 5.3%. As buyers look for essential chemical equipment, understanding their needs becomes paramount.
One vital category includes reactors. They facilitate crucial chemical reactions and vary by process requirements. The demand for highly efficient reactors is on the rise, driven by needs for higher yields and lower energy consumption. Additionally, separators play a critical role in purifying substances and separating components, a necessity for maintaining product quality.
Pumps, another essential equipment, are vital for fluid transport in chemical operations. Industry standards highlight the need for pumps that offer reliability and energy efficiency. Moreover, heat exchangers are critical in controlling temperatures during chemical reactions. However, selecting the right type can be challenging, as inefficiencies can lead to increased costs and operational delays. Buyers must weigh specifications against their operational requirements.
Understanding the Global Market for Chemical Equipment and Its Trends
The global market for chemical equipment is rapidly evolving. According to a recent market analysis, the chemical equipment industry is projected to reach $300 billion by 2025. This growth is driven by increasing demand in sectors like pharmaceuticals, petrochemicals, and food processing. Emerging economies are key players, expanding their chemical production capabilities to meet rising local and global demands.
Technological advancements are reshaping the market landscape. Automation and digitalization are enhancing efficiency in chemical manufacturing. However, challenges remain. Companies must navigate regulatory compliance, sustainability issues, and supply chain disruptions. A report by Grand View Research highlights that nearly 45% of chemical equipment manufacturers are investing in green technologies. The shift towards eco-friendly practices reflects growing consumer preferences for sustainable products.
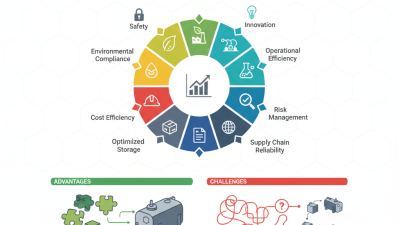
Understanding these trends is crucial for global buyers. They should assess the reliability and expertise of suppliers. Research indicates that quality packaging for chemical products can improve safety and operational efficiency. Buyers must stay informed about market dynamics. The ability to adapt to changes can differentiate successful players in this competitive industry.
Key Types of Chemical Equipment Crucial for Manufacturing Processes
Chemical manufacturing relies heavily on specialized equipment. A few key types provide essential functions in various processes.
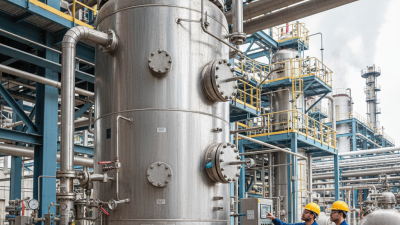
Reactors are at the forefront, enabling chemical reactions under controlled conditions. Their design varies widely based on reaction type. Some are stirred,
while others use a fixed bed approach.
Heat exchangers are vital for managing temperature. They transfer heat between two fluids, optimizing energy use.
This equipment requires careful construction to withstand high pressures and corrosive substances. Additionally,
separators play a significant role in distillation and purification. They separate components based on differences in physical properties, aiding in product refinement.
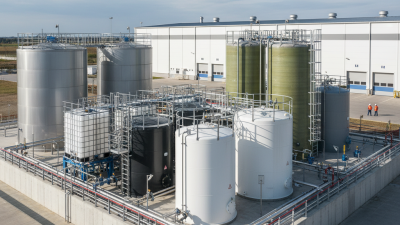
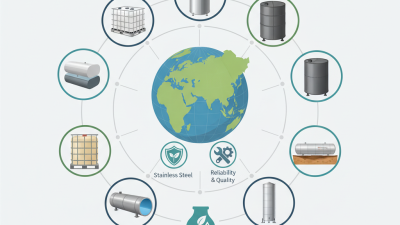
Storage tanks ensure safe containment of chemicals. Their capacity and materials depend on the nature of the substances.
Safety is crucial; leaks and spills can have severe consequences. Pumps also play a key role in the movement of fluids.
They must be chosen based on flow requirements and chemical compatibility. Understanding these factors can lead to improved efficiency and safety in manufacturing processes.
However, making the right choices requires expertise and reflection on past experiences.
Innovative Technologies Shaping the Future of Chemical Equipment
Innovative technologies are transforming the landscape of chemical equipment. Automation is at the forefront, minimizing human error and enhancing efficiency. Smart sensors are increasingly used, providing real-time data on processes. This leads to better control and optimization of operations.
However, integration challenges often arise with existing systems.
Another significant advancement is in materials science. New, durable materials are being developed, which can withstand extreme conditions. This reduces maintenance costs and downtime. Despite these improvements, the transition can be slow and costly for many companies.
Sustainability is gaining traction. Equipment designed for energy efficiency helps lower the carbon footprint. However, the initial investment remains a barrier for some buyers. Effective training for operators is also crucial to harness these innovations fully. Challenges like these highlight the complex nature of adopting new technologies in the chemical industry.
Regulatory Standards Impacting Chemical Equipment Procurement Globally
In the realm of chemical equipment procurement, understanding
regulatory standards is crucial. Various global regulations dramatically impact
purchasing decisions. For instance, the International Organization for Standardization (ISO)
recommends adherence to safety and environmental standards. These directives help ensure equipment quality
and safety.
A recent report from the Chemical Engineering Association indicated
that over 30% of procurement teams face difficulties
in aligning with evolving regulations. This statistic highlights the importance of staying informed. When
regulations change, the implications for compliance can lead to significant delays and additional costs.
It's essential to monitor industry updates regularly
to avoid being caught off guard.
Tip: Establish relationships with regulatory bodies to
receive updates. These connections can provide insights into upcoming changes that could affect procurement
processes.
Another critical aspect is the regional differences
in regulations. In some countries, stringent laws exist for hazardous materials that may not be present elsewhere.
This can create challenges for global buyers. Understanding the specific requirements for each region is vital
for compliance and functionality.
Tip: Create a checklist of regional regulations. This simple tool
can streamline compliance efforts and reduce oversight risks.
Navigating the complexities of regulatory standards is not just a requirement but a necessity for successful
procurement strategies in the chemical equipment sector.
Conclusion
The article "Top 10 Essential Chemical Equipment for Global Buyers" provides a comprehensive overview of the critical equipment necessary for the chemical manufacturing industry. It explores the global market trends influencing chemical equipment procurement, highlighting the key types of machinery pivotal for various manufacturing processes. Additionally, the article delves into innovative technologies that are shaping the future of chemical equipment, emphasizing how advancements can enhance efficiency and sustainability.
Moreover, the discussion includes important regulatory standards that buyers must consider when sourcing equipment globally, ensuring compliance and safety. Lastly, the article presents cost analysis and budgeting strategies to help purchasers make informed decisions regarding their chemical equipment investments, ultimately supporting successful manufacturing operations in a competitive market.